- Loading...
I have seen visually strong collections lose coherence because the selected hardware supplier understood the drawing but not the brand position behind it.
A custom metal hardware supplier matches a fashion brand when its design judgment, production standards, commercial model, and repeat-order controls can consistently support the brand’s intended price tier, product experience, and visual identity.
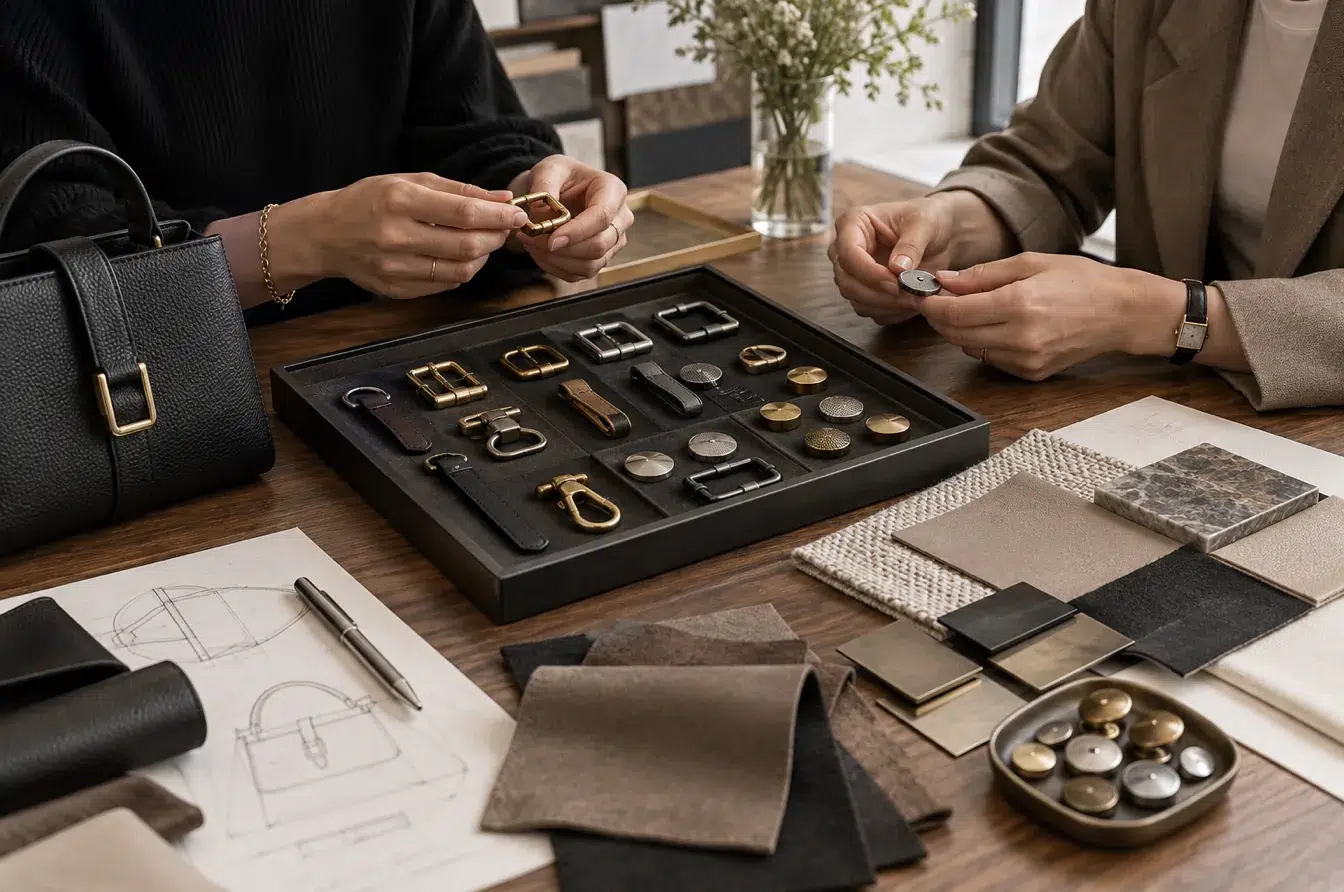
Supplier fit is not proved by a large catalogue, a polished presentation, or one attractive sample. It becomes visible when the supplier’s normal way of developing, producing, checking, and servicing hardware matches the way the brand creates and sells its products.
Which Brand Positioning Criteria Should Be Defined Before Evaluating a Metal Hardware Supplier?
Words such as premium, minimalist, technical, or accessible mean little until they are converted into decisions that a supplier can understand and reproduce.
A brand should define its target price tier, design language, tactile expectations, functional priorities, assortment structure, launch rhythm, and acceptable variation before comparing suppliers. These criteria turn positioning into a practical hardware brief and prevent quotations based on incompatible assumptions.
Translate Abstract Positioning Into a Hardware Brief
Brand positioning should first be expressed through the product experience. A quiet-luxury handbag may require restrained logo scale, controlled weight, softened edges, low-gloss finishing, and smooth mechanical movement. A rugged workwear collection may value stronger visual mass, practical attachment, repairability, and finishes that age without appearing defective. A directional fashion line may accept more complex geometry or unusual surface contrast, but development flexibility and precise execution become more important.
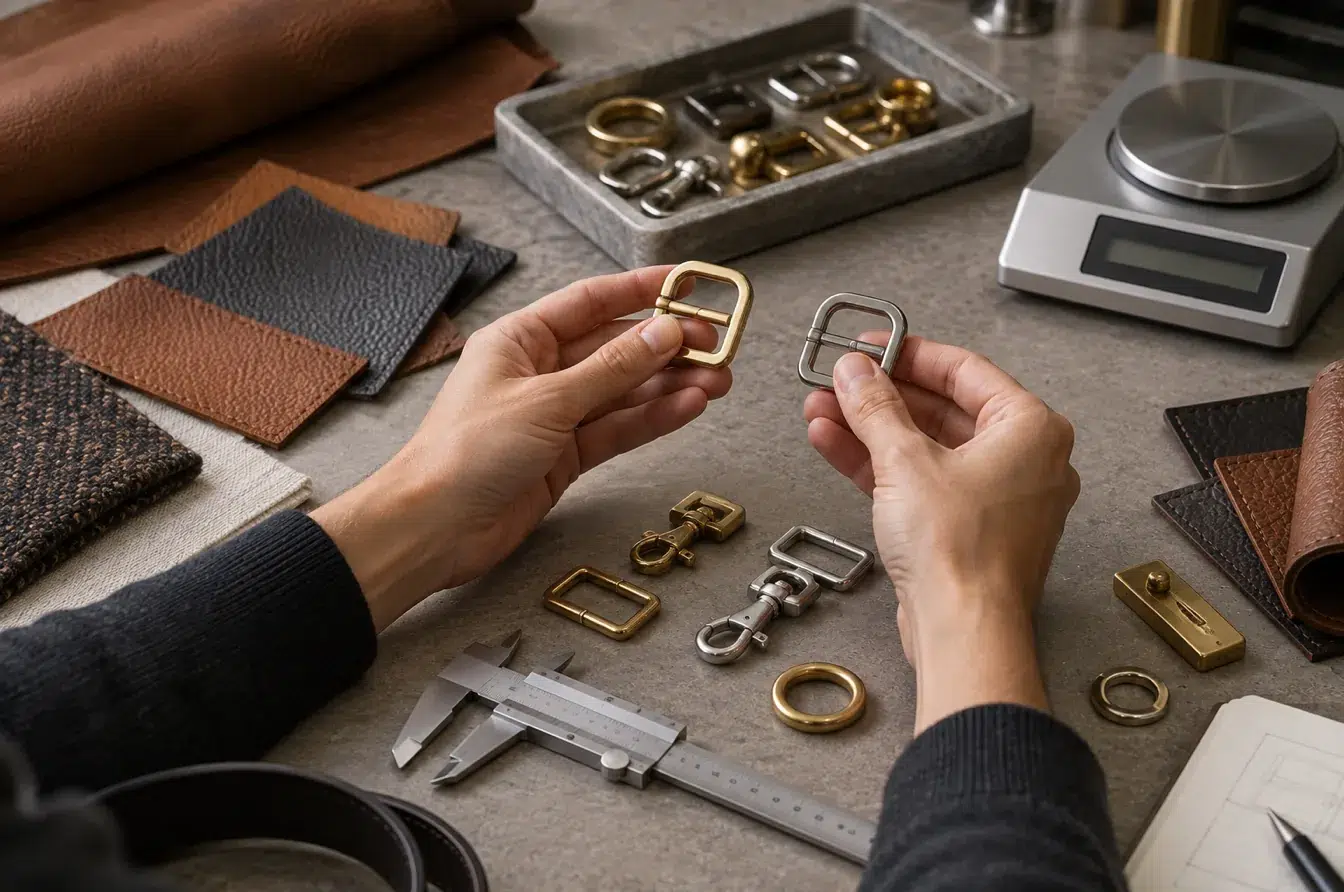
These choices need to enter the brief as observable or measurable requirements. The document should identify the component’s application, visible surfaces, approximate dimensions, preferred weight, base-material direction, color family, gloss level, texture, logo treatment, attachment method, movement, contact with fabric or leather, and expected use conditions. Reference products and mood boards can communicate the visual direction, but drawings, physical samples, and written acceptance points are needed to control production.
A supplier cannot demonstrate alignment with an undefined target. When the brand has not resolved whether the hardware should feel delicate, substantial, decorative, industrial, or nearly invisible, each candidate will interpret the project through its own catalogue and production habits. The comparison then measures different assumptions rather than supplier suitability.
| Positioning element | Hardware expression | Briefing question |
|---|---|---|
| Price tier | Material, weight, finish depth, detail resolution | What physical cues must support the intended retail value? |
| Design language | Proportion, geometry, logo scale, texture | Which details make the component recognizably part of the collection? |
| Product experience | Touch, movement, sound, edge comfort | How should the hardware feel during normal use? |
| Assortment strategy | Shared finishes, sizes, and component families | Which elements must remain consistent across styles? |
| Brand distinctiveness | Custom tooling, exclusive forms, controlled reuse | Which features must not become generic? |
Set Priorities Before Comparing Suppliers
Not every criterion should carry equal weight. A limited-run accessories label may place greater value on development support, low-volume flexibility, mixed finishes, and rapid design iteration. A scaled apparel program may prioritize stable repeat orders, clear specifications, delivery discipline, and the ability to coordinate several components for one collection. A premium leather-goods brand may treat finish depth, logo clarity, edge quality, mechanical feel, and tool ownership as non-negotiable.
A simple weighted scorecard keeps these priorities visible. Design fidelity, category experience, material and finish control, development process, bulk consistency, commercial fit, communication, and repeat-order management can be scored separately. The weighting should be decided before quotations arrive so an attractive price does not quietly replace the original selection logic.
The scorecard should also distinguish a minimum requirement from a preference. A particular attachment geometry may be essential because the component must fit an existing leather construction. A specific gold tone may be preferred but still open to physical comparison. Separating these categories helps suppliers propose workable alternatives without weakening the design intent.
The result is not a universal definition of a good supplier. It is a definition of the right supplier for one brand, one product category, and one commercial stage. That distinction prevents a technically capable factory from being selected for a program that does not fit its normal operating model.
What Does a Supplier’s Customer Portfolio Reveal About Its Market Positioning?
A portfolio can look impressive while hiding whether the supplier normally serves businesses with the same product level, quantities, development pace, and expectations.
A supplier’s customer mix reveals the operating environment it is built to support. Comparable product categories, order profiles, customization depth, and repeat-order patterns are more informative than famous names or the total number of catalogue items.
Read the Portfolio as an Operating Pattern
The portfolio should be examined for patterns rather than individual logos. A supplier working mainly with large garment factories may be highly effective at standardized components, scheduled volume, and price control. That model can suit established programs, but it may offer limited room for repeated design exploration or very small color runs. A studio serving independent designers may be comfortable with sketches, mood boards, and low-volume development, yet its production system may not be prepared for large replenishment orders.
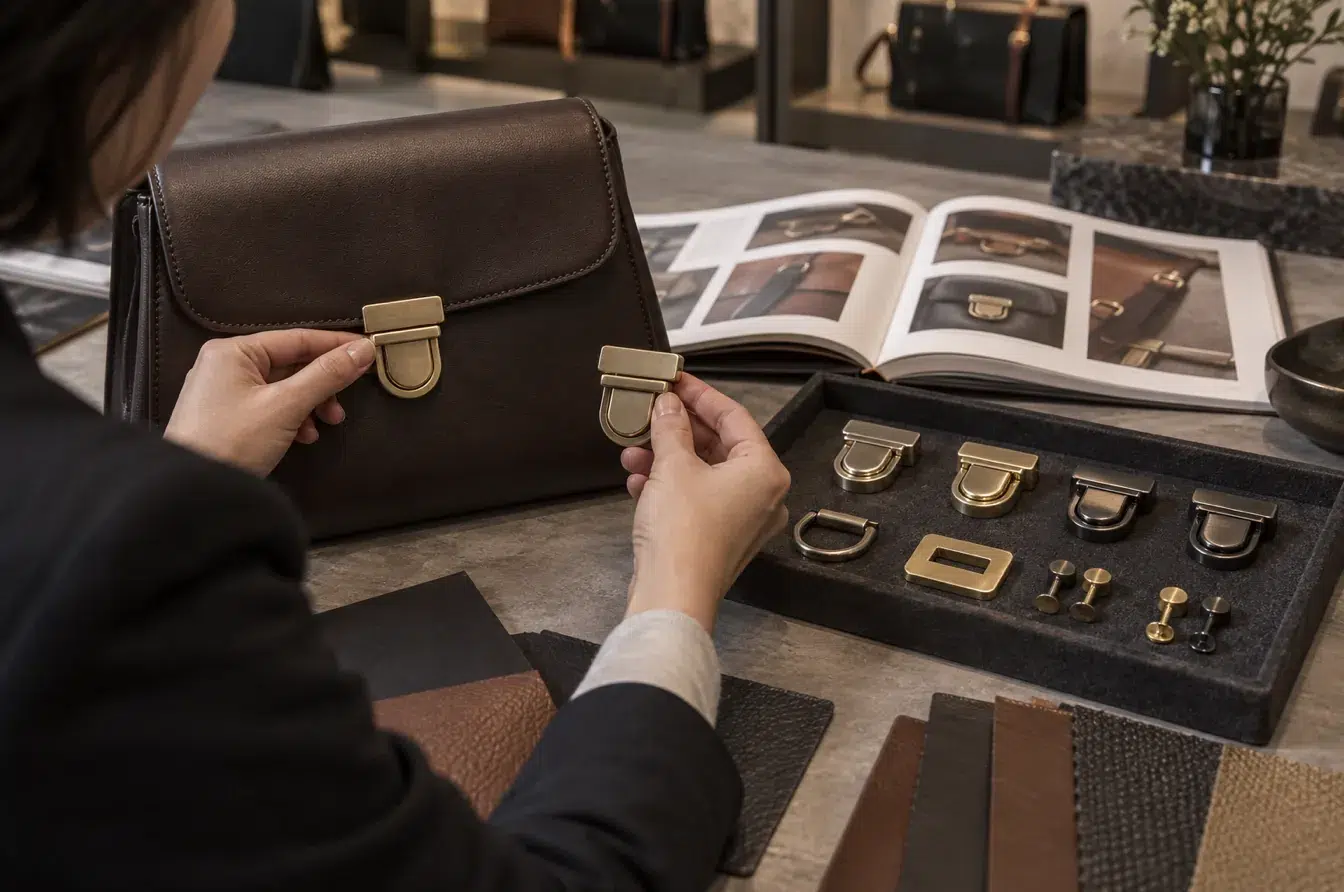
Product-category concentration also matters. Experience with small decorative logo plates does not automatically prove competence in moving clasps, structural buckles, zipper components, or hardware attached to delicate fabric. Comparable applications indicate that the supplier has already encountered similar decisions about geometry, attachment, finishing access, assembly, handling, and visible defect limits.
The strongest portfolio evidence connects a finished piece to the way it was developed. Useful examples show the starting brief, the supplier’s technical questions, the sample revisions, the production route, and the controls used for repeat orders. Even when client identities remain private, anonymized projects can still demonstrate relevant experience. The goal is not to collect prestigious names. It is to determine whether the supplier’s daily work resembles the proposed program.
| Portfolio pattern | Likely operating strength | Point to verify |
|---|---|---|
| Large apparel programs | Standardization, capacity, scheduled delivery | Flexibility for custom details and small variants |
| Independent designer projects | Iterative development and smaller launches | Ability to scale without changing the approved result |
| Premium leather goods | Finish control, tactile quality, mechanical detail | Experience with the exact component and attachment type |
| Broad multi-category supply | Consolidated purchasing and coordination | Depth of control within each individual process family |
| Repeated seasonal programs | Record retention and reorder continuity | Change control for materials, tools, and finishes |
Ask for Comparable Projects, Not Famous Clients
Well-known customer names can create confidence, but they rarely explain what the supplier actually produced. A factory may have supplied a simple stock ring through another manufacturer while presenting the relationship as evidence of advanced custom development. The useful question is not who purchased something. It is what component was made, which processes were controlled, what quantity pattern was involved, and how closely the project resembles the current requirement.
A comparable case should match several dimensions: product family, base material, manufacturing route, finish type, attachment, visual standard, quantity range, and replenishment pattern. Exact identity is unnecessary when confidentiality applies. Photographs of non-confidential samples, redacted drawings, process records, retained finish references, and explanations of sample changes can provide more practical evidence.
The discussion itself also reveals positioning. A suitable supplier should understand why a designer may protect a signature proportion, why a controlled antique effect cannot look randomly damaged, or why identical gold tones across several components matter to one collection. If every project is reduced immediately to size, quantity, and unit price, the supplier may be treating the hardware as a generic item rather than part of the brand language.
Customer concentration should also be considered. A brand with frequent small reorders may receive limited attention from a supplier organized around a few very large accounts. Conversely, a small workshop may give excellent development support but struggle when one customer expands rapidly. Portfolio fit therefore concerns both creative relevance and operational balance.
Do the Supplier’s Design, Material, and Finish Standards Match the Brand’s Price and Quality Tier?
An attractive rendering or showroom sample can conceal substitutions, simplified details, and finishing limits that become obvious only after the hardware reaches the final product.
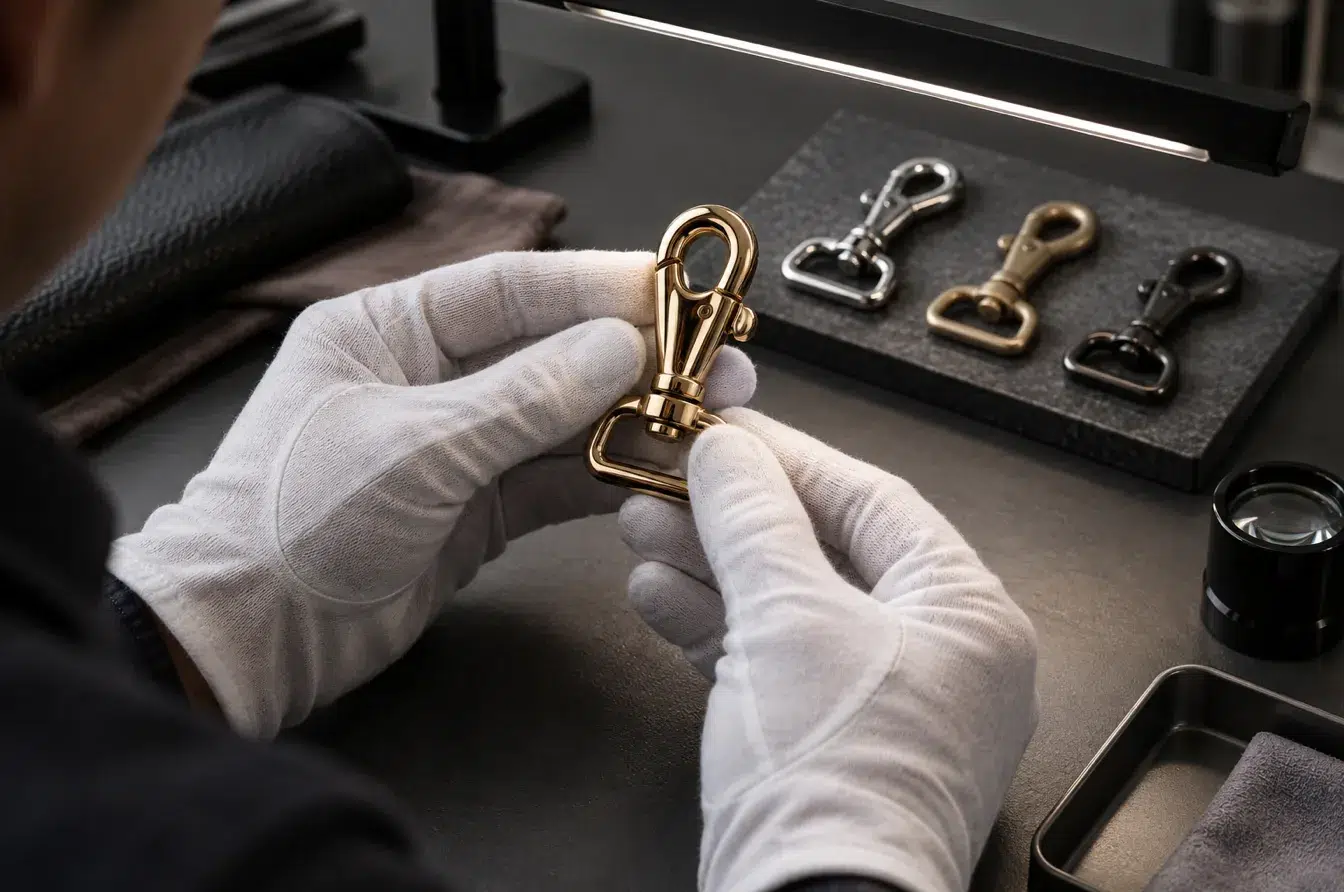
The match should be judged through the complete component: geometry, base material, weight, edge condition, attachment, movement, surface preparation, color, gloss, texture, and batch repeatability. Every choice should support the intended product experience and remain practical in production.
Connect Design Language to Production Choices
The same logo can become a thin stamped plate, a heavier cast emblem, an engraved component, an enamel-filled badge, or a subtle laser mark. Each route changes the visual depth, edge character, weight, cost, and way the part interacts with the final product. A supplier aligned with the brand should explain these consequences before tooling begins.
Material choice should follow both appearance and application. Weight can create a sense of substance on a handbag but distort a lightweight garment. A highly reflective finish can support a bold luxury direction but expose polishing waves, scratches, and uneven surfaces. A matte finish may look restrained, yet inconsistent preparation can produce cloudy areas or visible handling marks. Complex geometry may strengthen recognition while making polishing, plating coverage, assembly, or attachment more difficult.
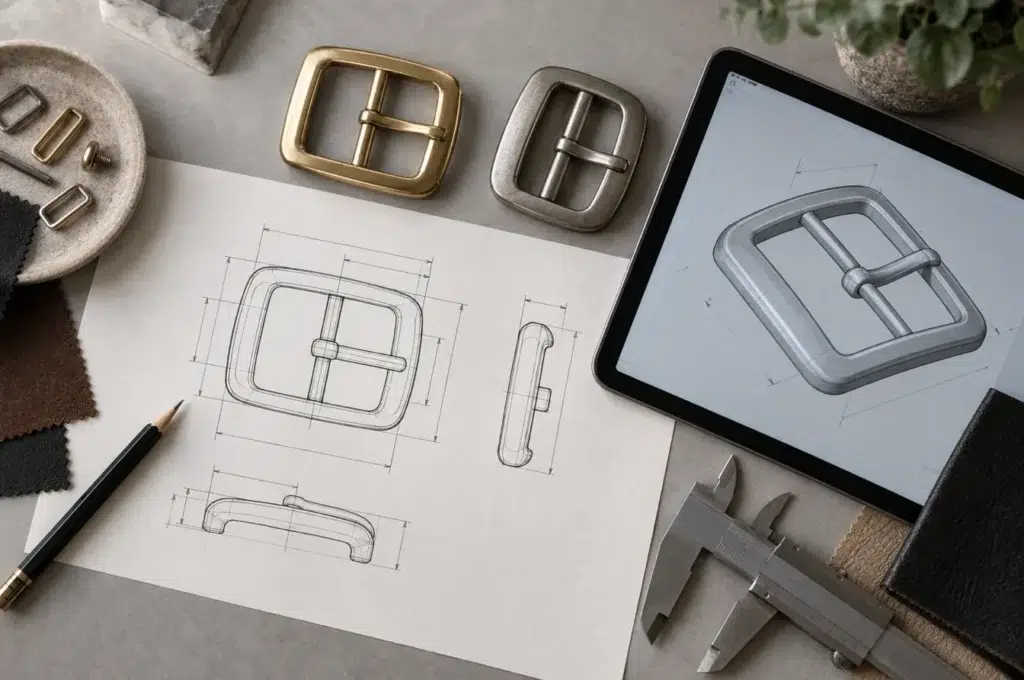
Design review should therefore include the hidden surfaces and interfaces, not only the front view. Rear posts, sewing holes, prongs, loops, hinge clearances, spring spaces, and backing plates determine whether the hardware can be attached cleanly and used comfortably. The strongest supplier response protects the visible intent while proposing practical changes to concealed structures. It should state which features are being preserved, which must change, and how each change affects the finished result.
| Design decision | Positioning effect | Production question |
|---|---|---|
| Base material and weight | Perceived substance, comfort, and balance | Does the material suit both the look and application? |
| Logo depth and edge definition | Brand recognition and visual precision | Can the detail survive tooling, polishing, and finishing? |
| Gloss and texture | Luxury, utility, vintage, or technical character | How will the approved surface be repeated by batch? |
| Attachment structure | Clean appearance and product reliability | Does the hidden construction suit the final substrate? |
| Tooling and reuse rules | Distinctiveness and design control | Who controls the tool and where may the design be reused? |
Evaluate the Total Program Cost Behind the Price Tier
Unit price alone cannot show whether a supplier supports the intended quality tier. Two quotations may cover different materials, polishing stages, finish preparation, inspection scope, assembly methods, protective packing, or sample revisions. The lower number may simply exclude work that will later appear as a defect, delay, or added charge.
The comparison should separate tooling, development samples, additional finish options, revision rounds, unit production, assembly, individual protection, packing, and delivery responsibilities. It should also state the assumptions behind the quotation. If the final weight, material, finish, or attachment remains open, the price is provisional even when the quotation looks precise.
Physical review is essential because price-tier signals are experienced through touch as well as sight. Weight distribution, edge softness, mechanical resistance, movement sound, backside cleanliness, and the interaction with leather or fabric cannot be judged reliably from digital images. A premium result may depend on small differences that do not appear in a basic specification.
The best-value supplier is therefore not automatically the lowest or most expensive. It is the supplier whose process includes the work needed to achieve the approved result with limited uncertainty. A transparent price structure makes that fit visible and allows the brand to decide where complexity adds value and where a simpler solution would be equally effective.
Do Its MOQ, Development Process, and Service Model Fit the Brand’s Business Model?
A supplier can produce the right component and still be the wrong partner when its minimums, workflow, decision speed, or reorder system conflict with the brand’s operation.
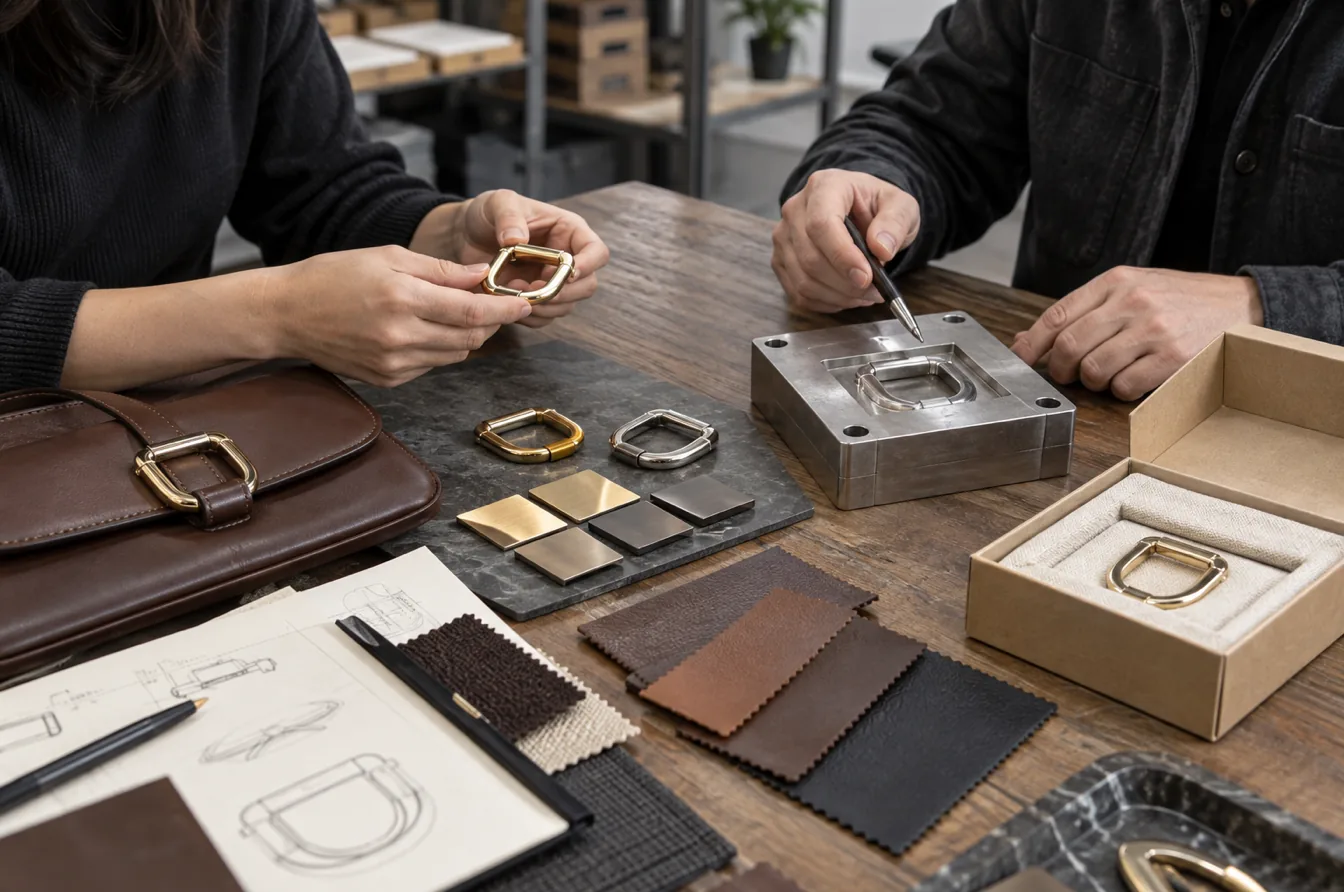
Commercial fit depends on how MOQ is calculated, how designs move from brief to approval, who owns each decision, and whether service remains effective as quantities change. The supplier’s normal workflow should match the brand’s collection calendar and internal resources.
Break MOQ Into Its Real Production Drivers
MOQ should be understood by design, size, material, finish, color, attachment, and packing configuration. A headline minimum may apply to one standard component, while each custom finish or logo variant carries its own batch requirement. Several pieces that look similar in a collection may still need separate setups, tools, finishing racks, or assembly work.
This structure affects brands differently. A limited-edition label may need several designs in small quantities and prefer a supplier that can combine compatible work or support controlled pilot runs. A continuity program may accept larger batches but require stable replenishment and retained specifications. A growing brand needs to know whether the process can move from launch quantities to higher volume without changing material, finish, factory route, or service quality.
Tooling must be reviewed alongside MOQ. Existing tools can reduce development cost when the component is not intended to be distinctive. Signature pieces may justify dedicated tooling, but the agreement should define ownership, storage, maintenance, modification, and reuse. MOQ, tooling, and design exclusivity are therefore connected decisions rather than separate purchasing terms.
| Commercial variable | Detail to clarify | Business-model implication |
|---|---|---|
| MOQ basis | Per design, size, finish, color, or total order | Determines real inventory exposure |
| Sampling structure | Included stages, options, and revision rules | Determines development cost and timing |
| Tooling arrangement | New or existing tool, ownership, maintenance, reuse | Affects differentiation and repeat orders |
| Replenishment | Minimum, retained references, and scheduling | Determines continuity after launch |
| Scaling path | Capacity and process control at higher volume | Shows whether growth can occur without quality drift |
Match the Service Model to Internal Resources
Some brands arrive with controlled drawings, defined tolerances, physical finish references, and an experienced product-development team. They may need a supplier that executes precisely, raises technical conflicts, and maintains disciplined revision records. Other brands begin with a sketch, logo, mood board, or reference product and need more support with structure, material, attachment, drawings, and sample planning.
Neither model is inherently better. The problem appears when expectations differ. A production-focused supplier may interpret incomplete information through familiar factory defaults. A development-led supplier may add time and cost that a fully specified program does not need. The brand should define which decisions remain internal and which decisions the supplier is expected to develop.
Communication should also follow a controlled route. One person should own commercial coordination, while technical comments should return to a current drawing, marked sample record, or approved specification. Verbal changes scattered across messages create uncertainty about which instruction controls production. Response speed matters, but decision accuracy and record quality are more important than an immediate answer.
Service fit continues after delivery. Repeat orders require retained drawings, finish references, packaging instructions, tool status, and a clear process for reporting changes. A supplier that performs well during an intensive first development but cannot preserve those records may weaken brand consistency over time. The operating model must support the entire product life, not only the first purchase order.
How Can Samples and a Trial Order Confirm the Supplier-Brand Fit?
One polished sample proves that a result was achieved once; it does not prove that the supplier can reproduce it through normal production and repeat orders.
Samples and trial orders should test design interpretation, revision control, process stability, communication, inspection, packing, and delivery together. The supplier-brand fit is confirmed only when the approved product and the operating process both perform as expected.
Turn the Approved Sample Into a Controlled Standard
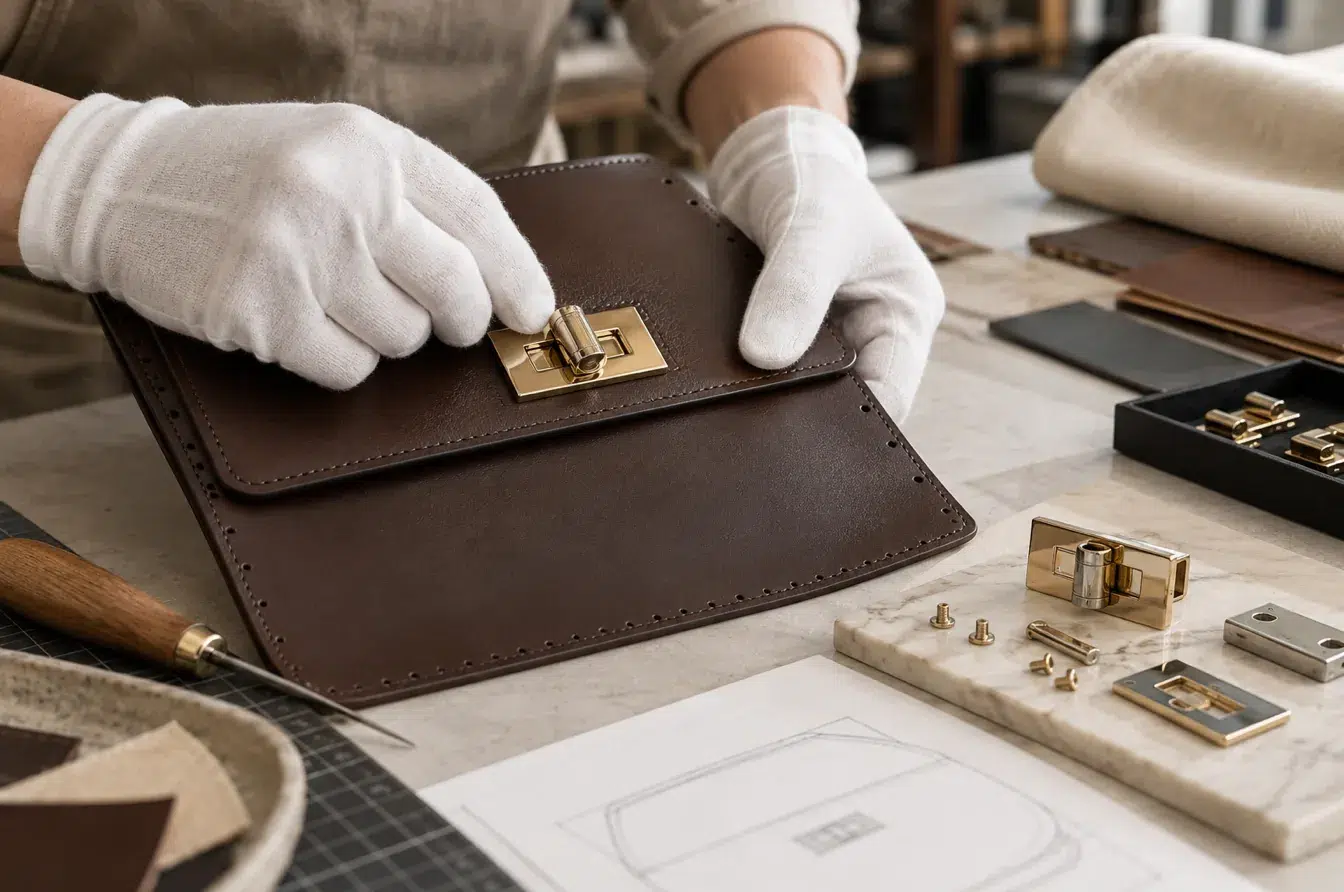
Sample approval should identify exactly what has been accepted. The record needs the part name or number, drawing revision, dimensions, base material, finish, color reference, gloss or texture, logo treatment, attachment, mating parts, packing method, and any agreed variation. A photograph can support the record, but it cannot replace the physical appearance or the current technical information.
Evaluation should occur on the intended product whenever possible. A buckle may look balanced on a table but feel too heavy on a lightweight garment. A logo plate may have clean front details but create pressure points or visible distortion after attachment. A zipper pull may appear refined yet interfere with the slider or make an unwanted sound during use. Application testing connects the hardware to the actual brand experience.
The review should also distinguish cosmetic, dimensional, and functional observations. Cosmetic approval covers color, gloss, texture, polishing, logo clarity, and visible defects. Dimensional approval covers fit, clearances, alignment, and critical interfaces. Functional approval covers movement, attachment, repeated operation, and interaction with the final material. Keeping these groups separate makes comments clearer and prevents a visual approval from being mistaken for full product approval.
| Approval area | What to review | Production reference |
|---|---|---|
| Appearance | Color, gloss, texture, logo, edges, visible surfaces | Approved physical sample and finish reference |
| Dimensions | Overall size, critical interfaces, clearances | Current controlled drawing |
| Function | Movement, attachment, fit, repeated use | Agreed product-specific check |
| Application | Balance, comfort, substrate interaction | Hardware installed on the intended product |
| Packing | Contact protection, orientation, quantity grouping | Approved packing instruction |
Use a Pilot Order to Test the Whole System
A pilot order should use normal production-intent tooling, materials, finishing, assembly, inspection, and packing. Its purpose is not merely to receive a smaller quantity. It tests whether the system that will make future orders can reproduce the approved standard without exceptional handling.
The comparison should include pieces from different positions within the batch, not only a hand-selected presentation set. Variations in color, gloss, polishing, casting detail, assembly, or movement may appear across production stages or finishing racks. The inspection plan should concentrate on the characteristics that carry the brand position: visible surface quality, logo consistency, tactile feel, mechanical behavior, and clean attachment.
Operational behavior is part of the trial. The brand can observe whether milestones are communicated, questions are raised before action, revisions are recorded, packing matches the agreement, and problems arrive with clear explanations and corrective options. A technically acceptable batch delivered through an unstable process may still signal poor long-term fit.
After the pilot, the final production package should be updated with every accepted decision. The approved sample, drawing, finish reference, inspection points, packing method, and reorder information should agree. A supplier that can preserve this controlled package is more likely to maintain the same product identity across seasons. The trial order then becomes evidence of repeatability rather than a one-time purchasing test.
Conclusion
The right supplier makes brand positioning reproducible through relevant experience, disciplined development, suitable commercial terms, controlled samples, and consistent execution from pilot order to reorder.